
Multi-spindle drilling · Case study
Six-Spindle Servo Drilling for PVC Parts
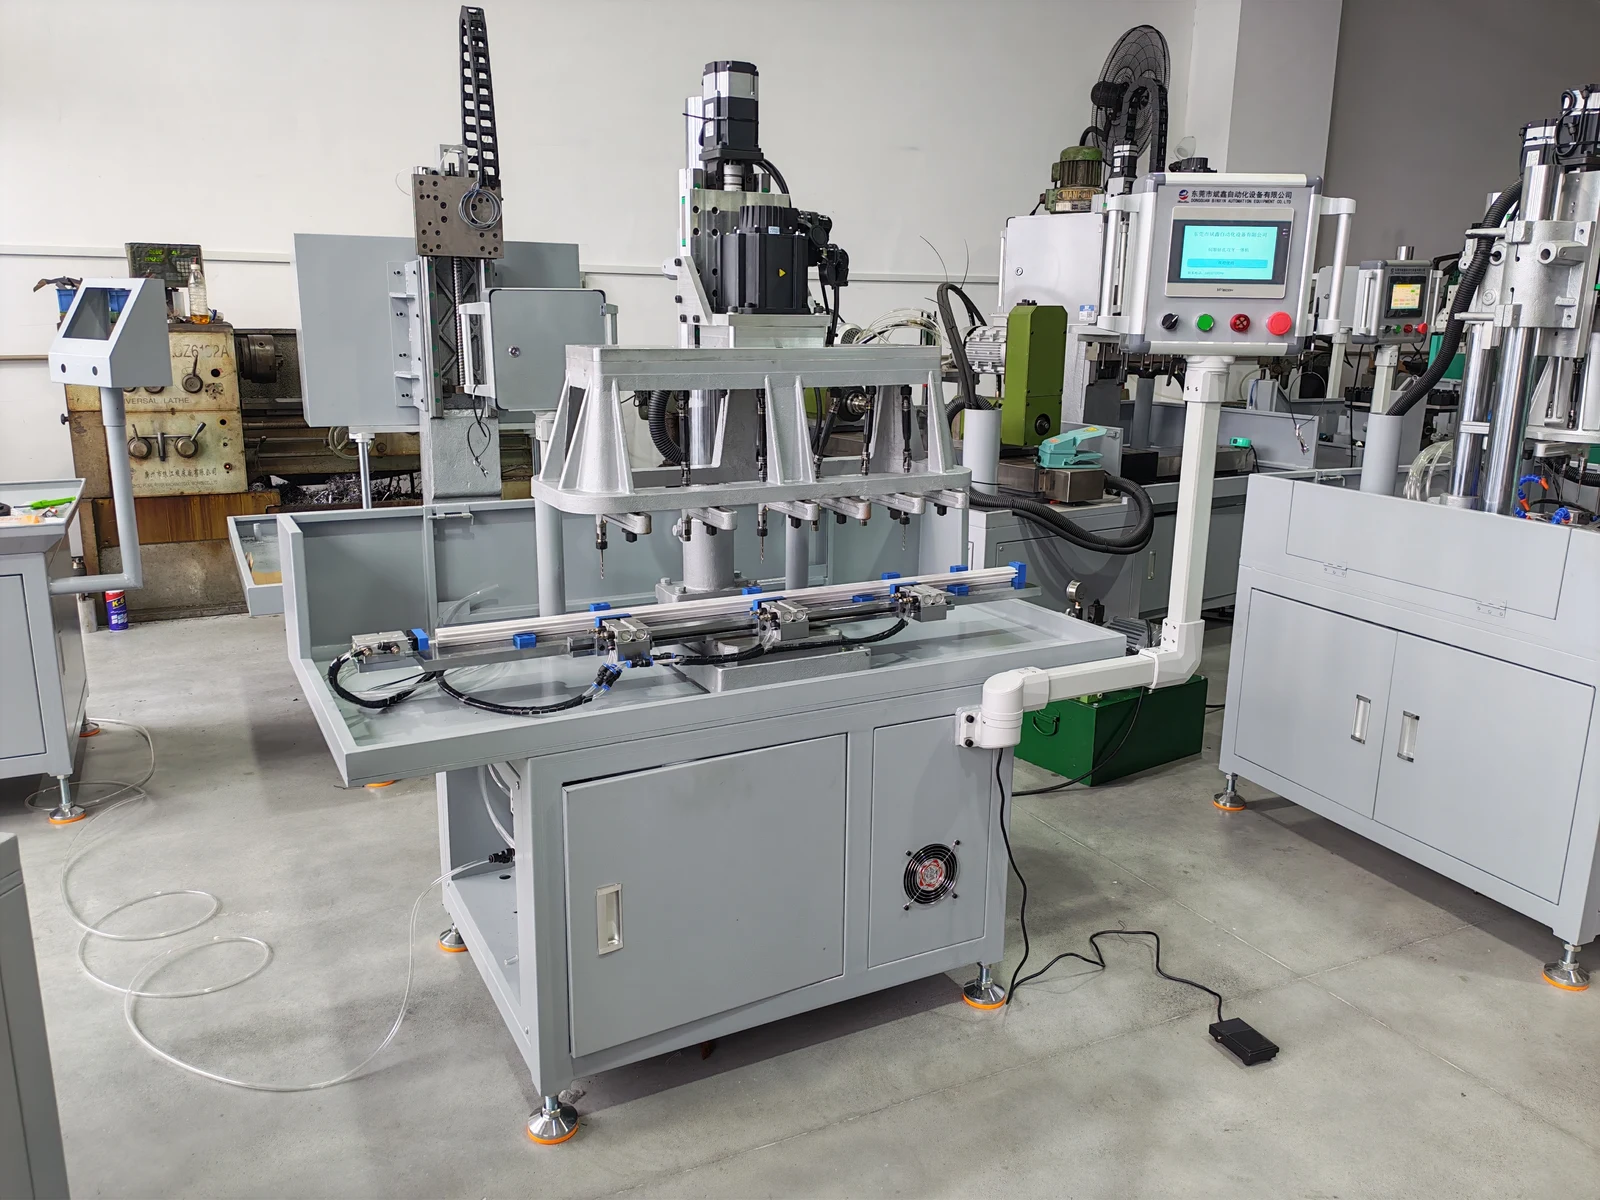
Drill multiple holes in a PVC part in one operation, with an adjustable setup for different part variants. The operator loads the fixture and removes each finished part; servo drives control spindle rotation and feed.
 View full-size image ↗
The customer's task
Use one adjustable setup for several PVC parts
The customer wanted several holes drilled at the same time, with adjustment for multiple PVC part variants and less labor required for production.
 View full-size image ↗
Match the hole pattern, then drill together
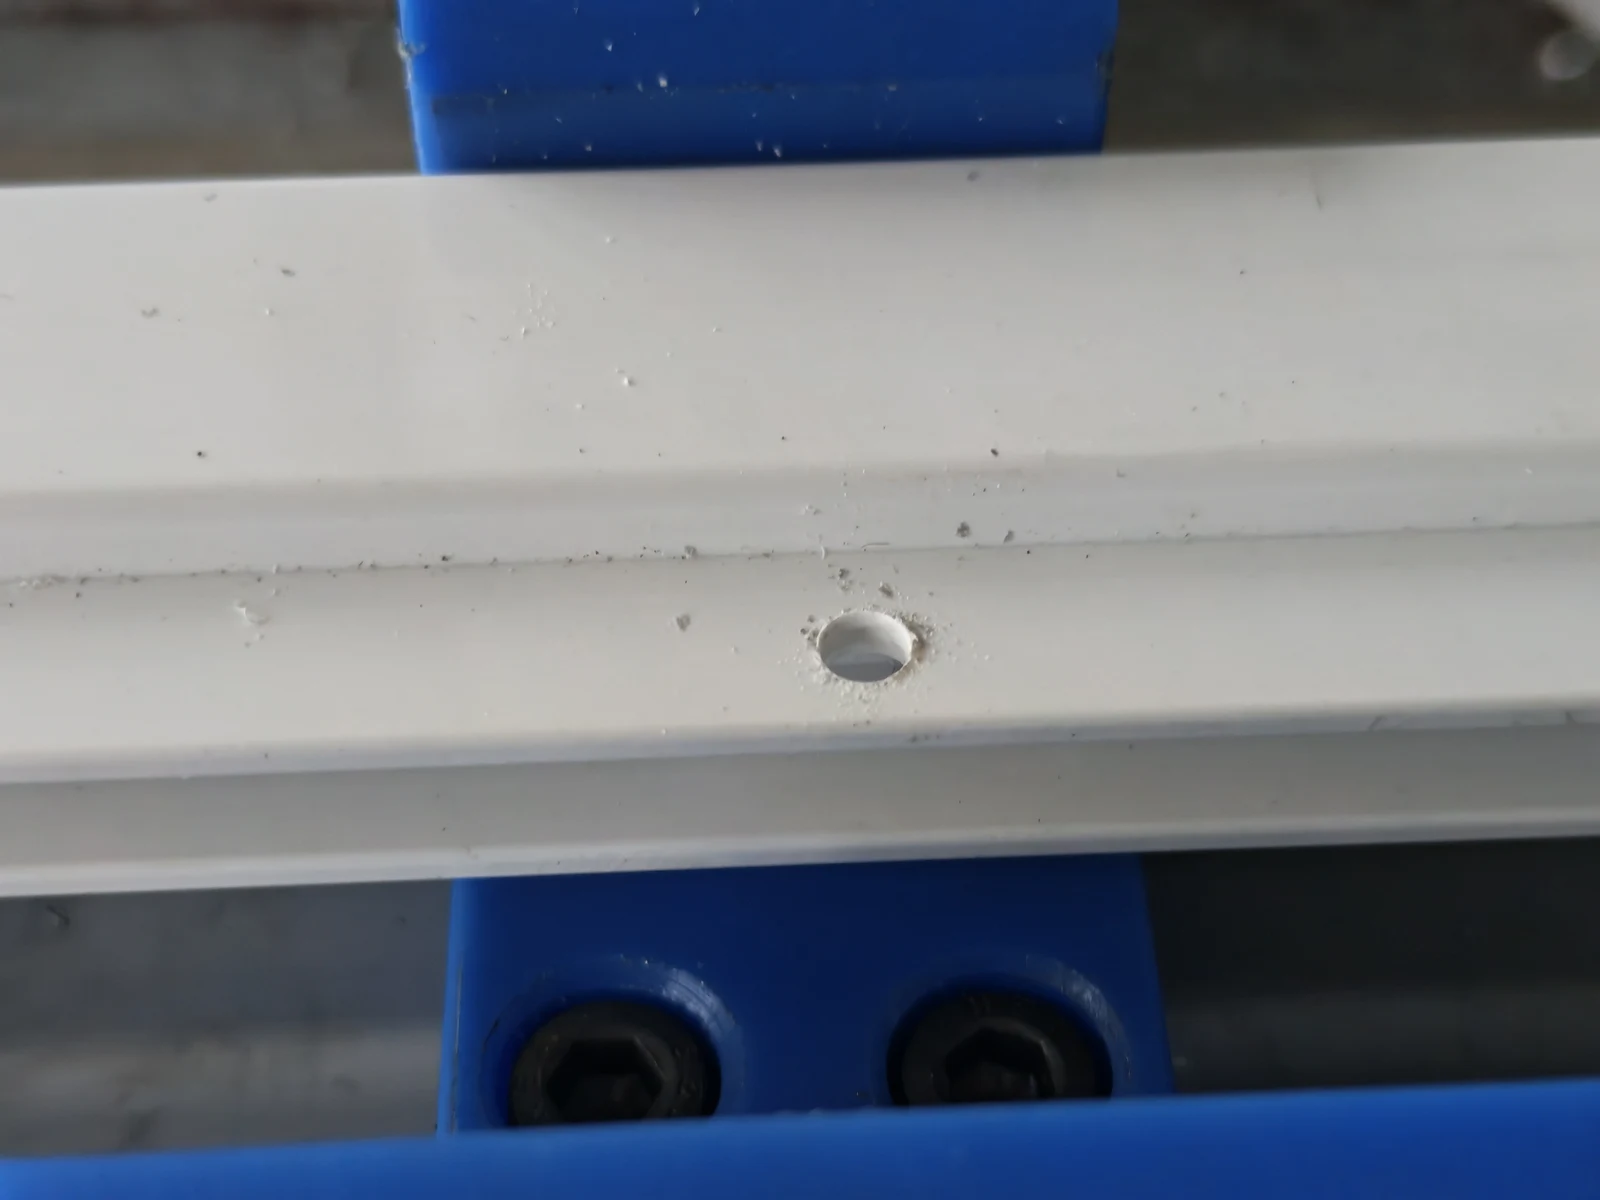
The specified parts range from 540 to 1184 mm in length and require holes from 3 to 5.5 mm in diameter. The six-spindle arrangement combines multiple drilling positions in the same operation.
The machine can be adjusted for the supplied part variants. The operator places the part in its fixture, starts the drilling operation and removes it after machining.
For your application, we review the length, cross-section and hole positions of each variant together. These details determine the fixture and spindle arrangement.
Workshop video
See the machine start and drill
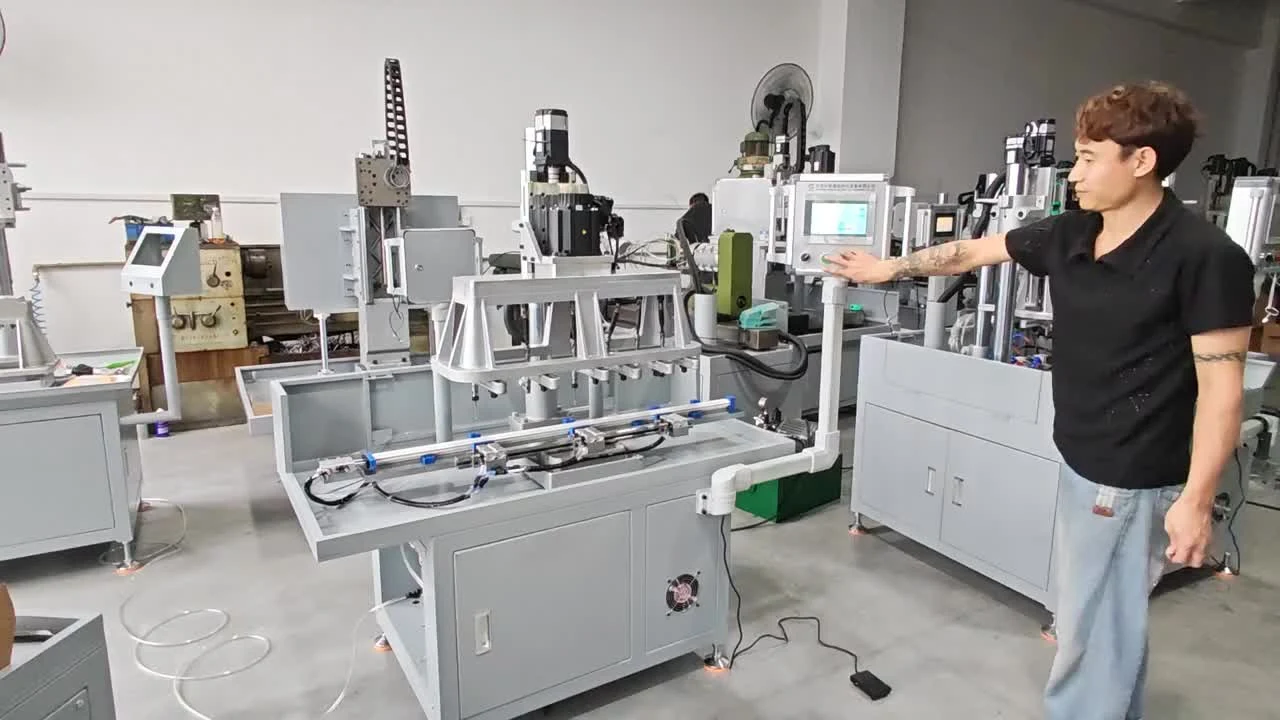
See the operator start the machine and the multi-spindle head drill at original operating speed.
Operating sequence
Manual handling with automatic multi-hole drilling
Load the workpiece
The operator places a PVC part in the fixture and locates it for drilling.
Start the operation
The operator starts the machine. PLC control coordinates the drilling sequence.
Drill the holes together
The multi-spindle head drills several holes in the same operation, with servo-driven spindle rotation and feed.
Remove and reload
After drilling is complete and the head retracts, the operator removes the part and loads the next one.
Machine configuration
Separate servo drives for rotation and feed
A 1.5 kW servo motor drives the spindle system. A separate 0.75 kW servo motor controls the feed, with PLC coordination and touchscreen parameter adjustment.
The fixture uses pneumatic-cylinder actuation. Loading and unloading remain manual; the adjustable setup accommodates the specified PVC part variants.
| Workpiece material | PVC |
|---|---|
| Workpiece length | 540–1184 mm |
| Drilling diameter | Ø3–5.5 mm |
| Spindle arrangement | Six spindles for simultaneous multi-hole drilling |
| Loading and unloading | Manual |
| Spindle motor | 1.5 kW servo motor |
| Feed motor | 0.75 kW servo motor |
| Fixture actuation | Pneumatic cylinder |
| Control system | PLC with touchscreen parameter adjustment |
| Electrical supply | 380 V |
| Machine dimensions | Approximately 1400 × 800 × 1700 mm |
| Machine weight | Approximately 200 kg |
Equipment and workpiece details
Inspect the fixture, tooling and machine layout
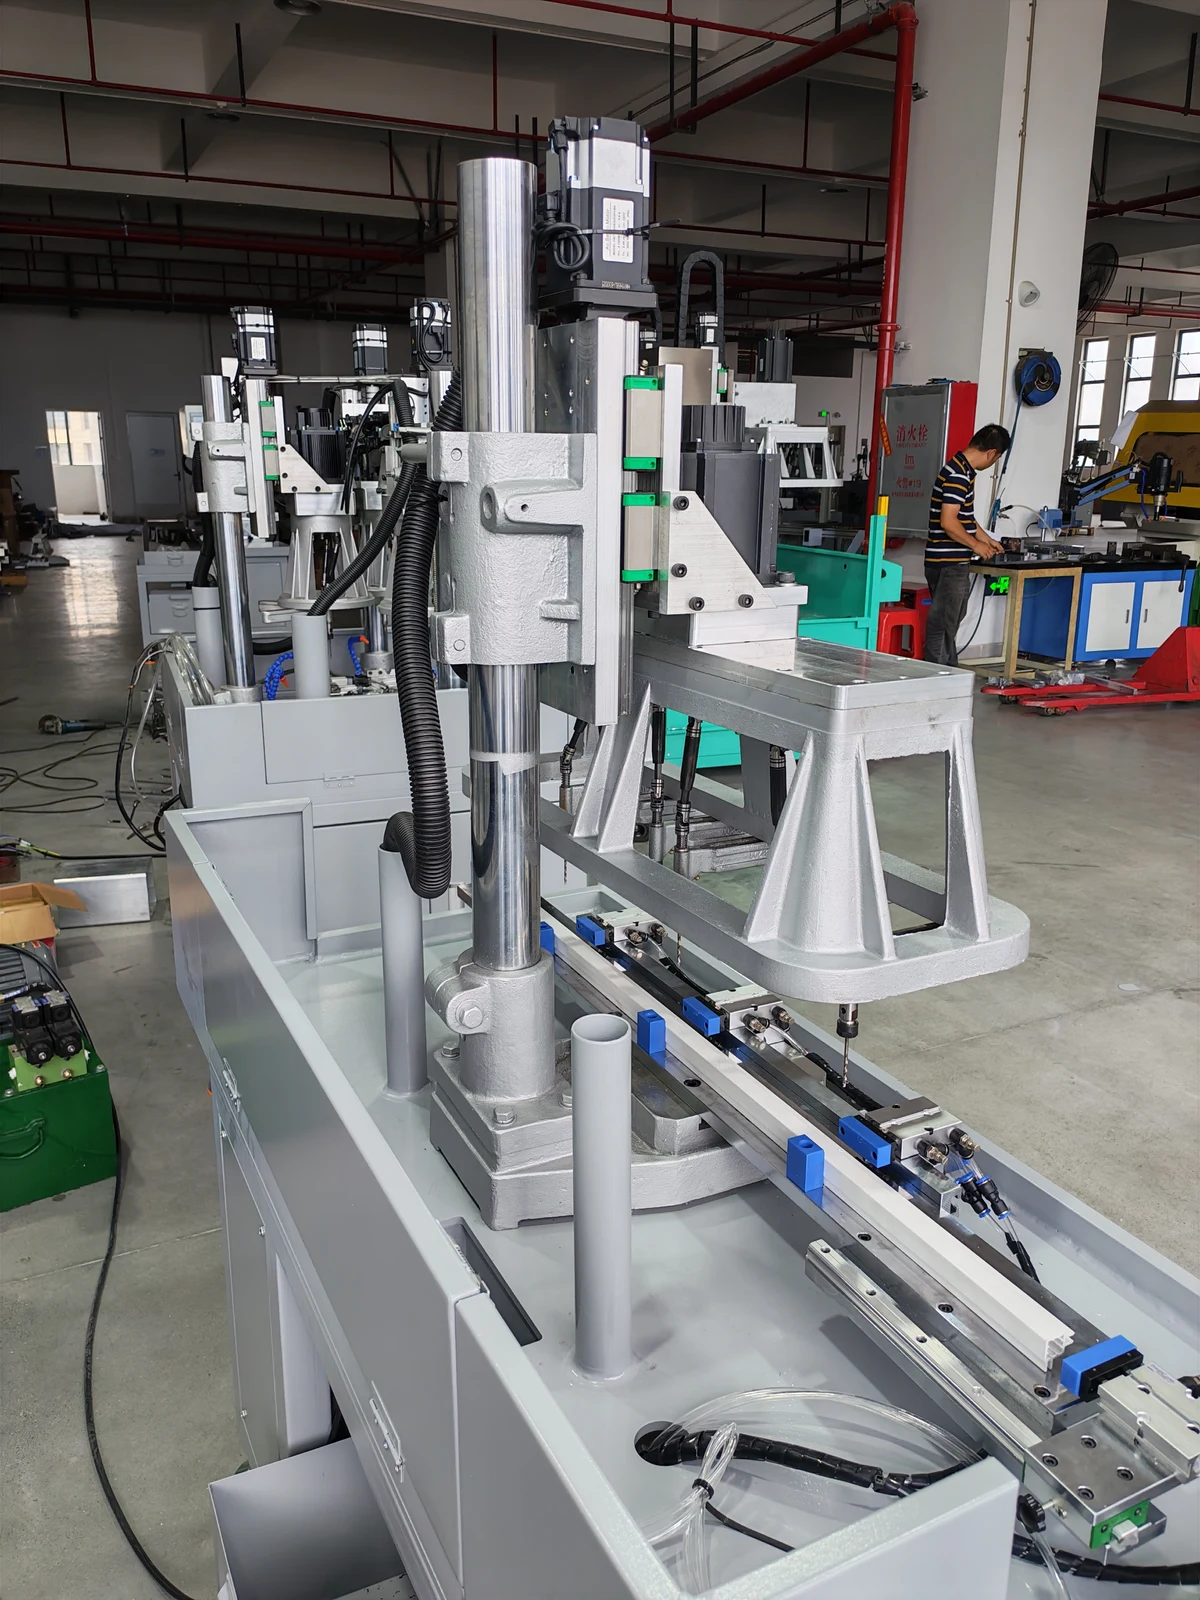
Selected photographs show distinct views of the machine and its working components. Open any photograph at full size.
 View full-size image ↗
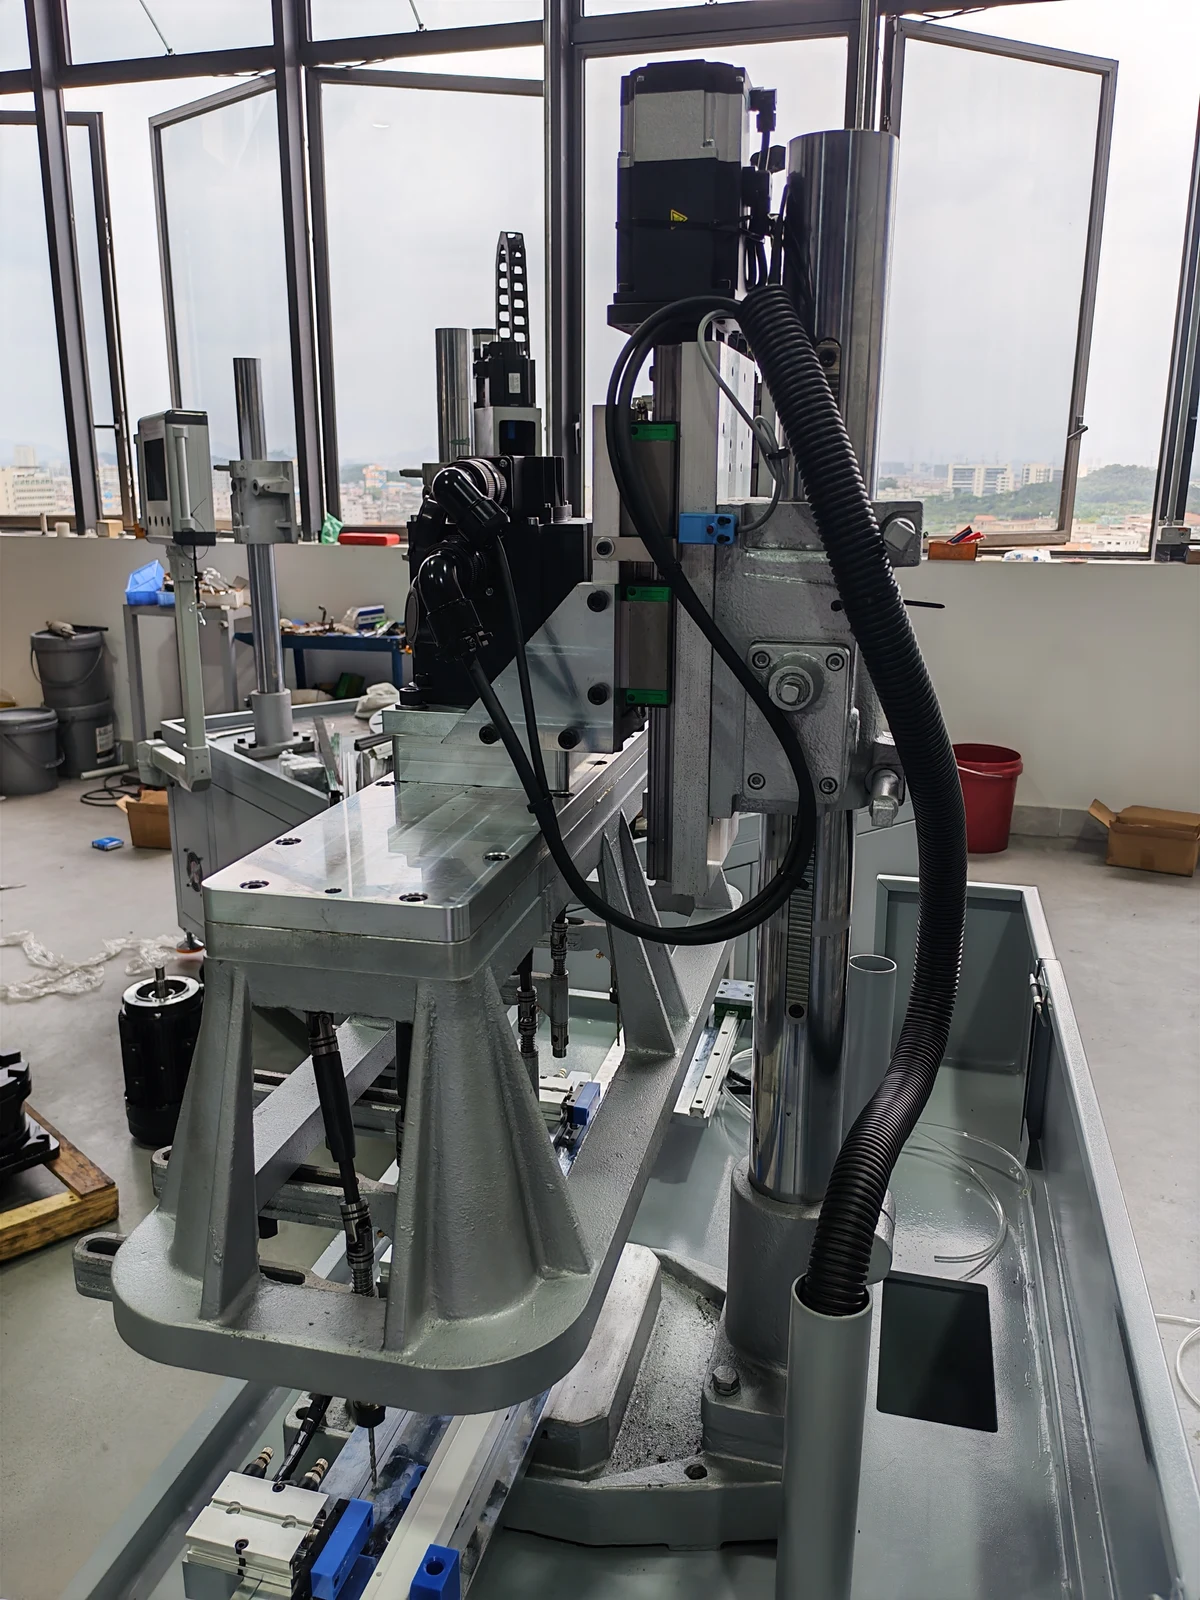
Side view
Side view of the column, feed assembly and workpiece fixture.
 View full-size image ↗
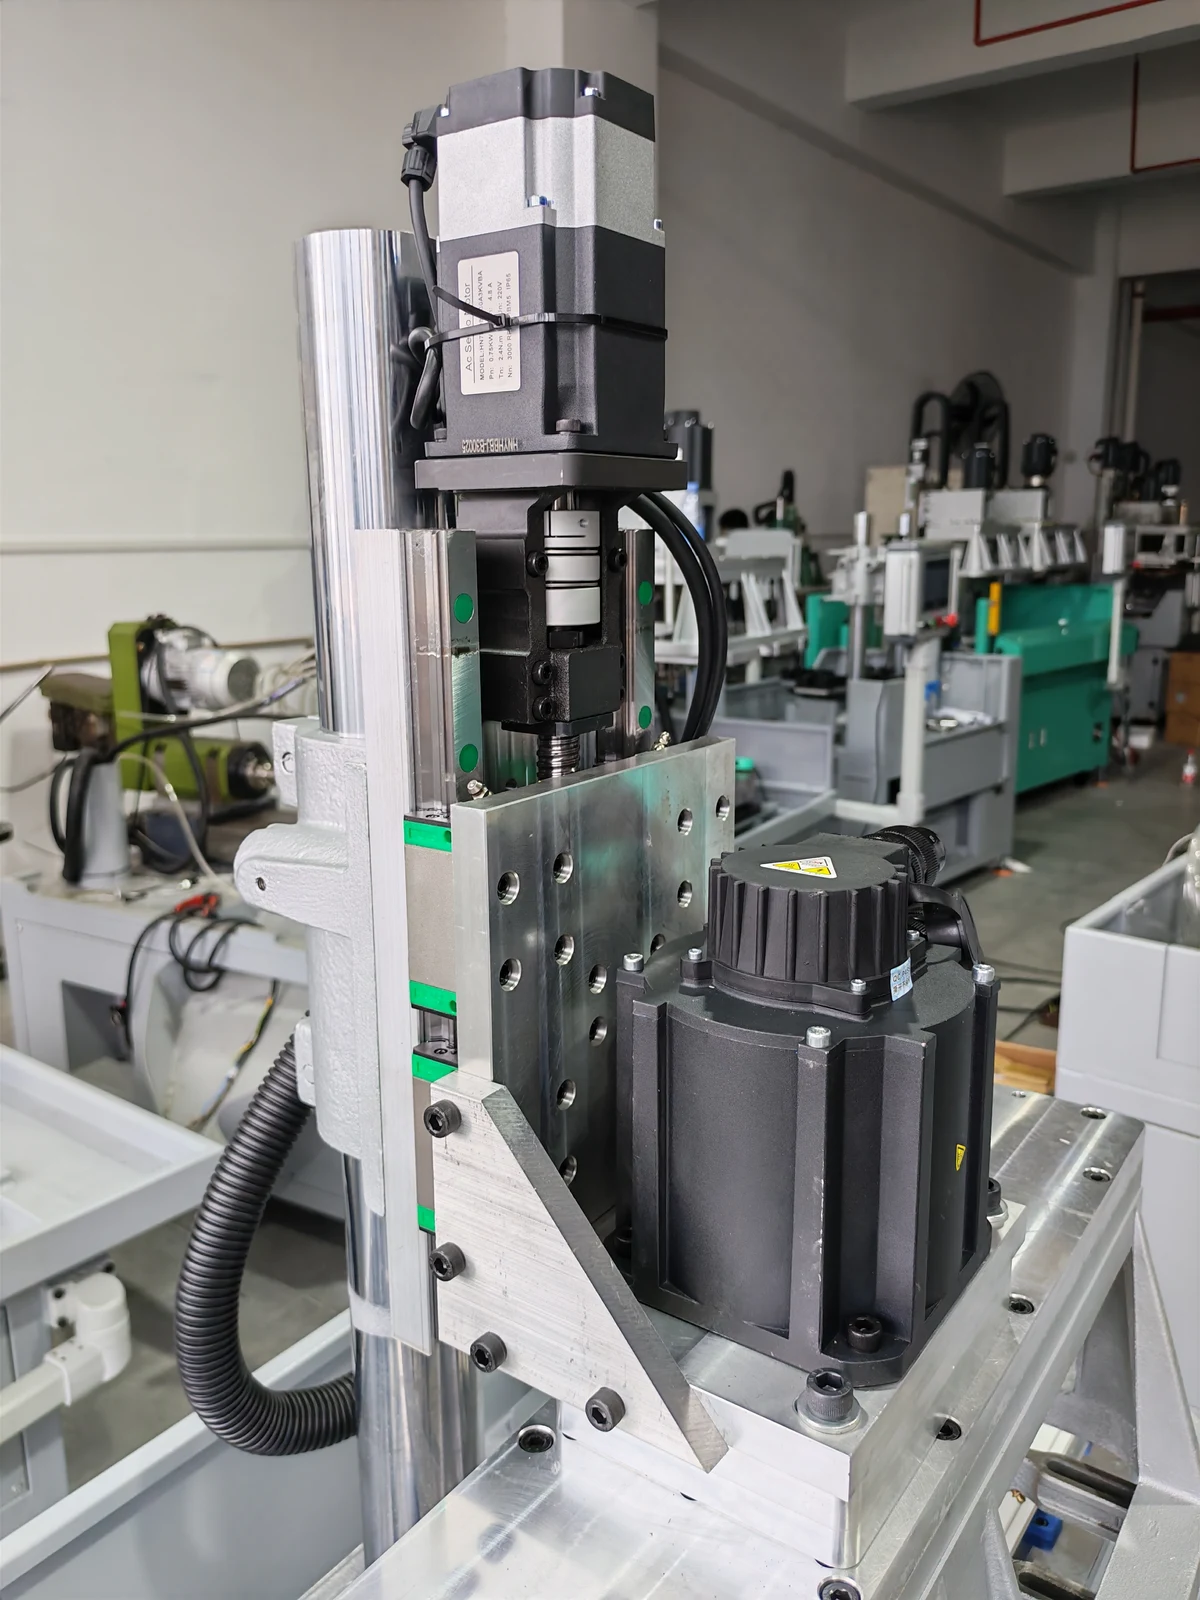
Rear view
Rear view of the head support and servo-drive cabling.
 View full-size image ↗
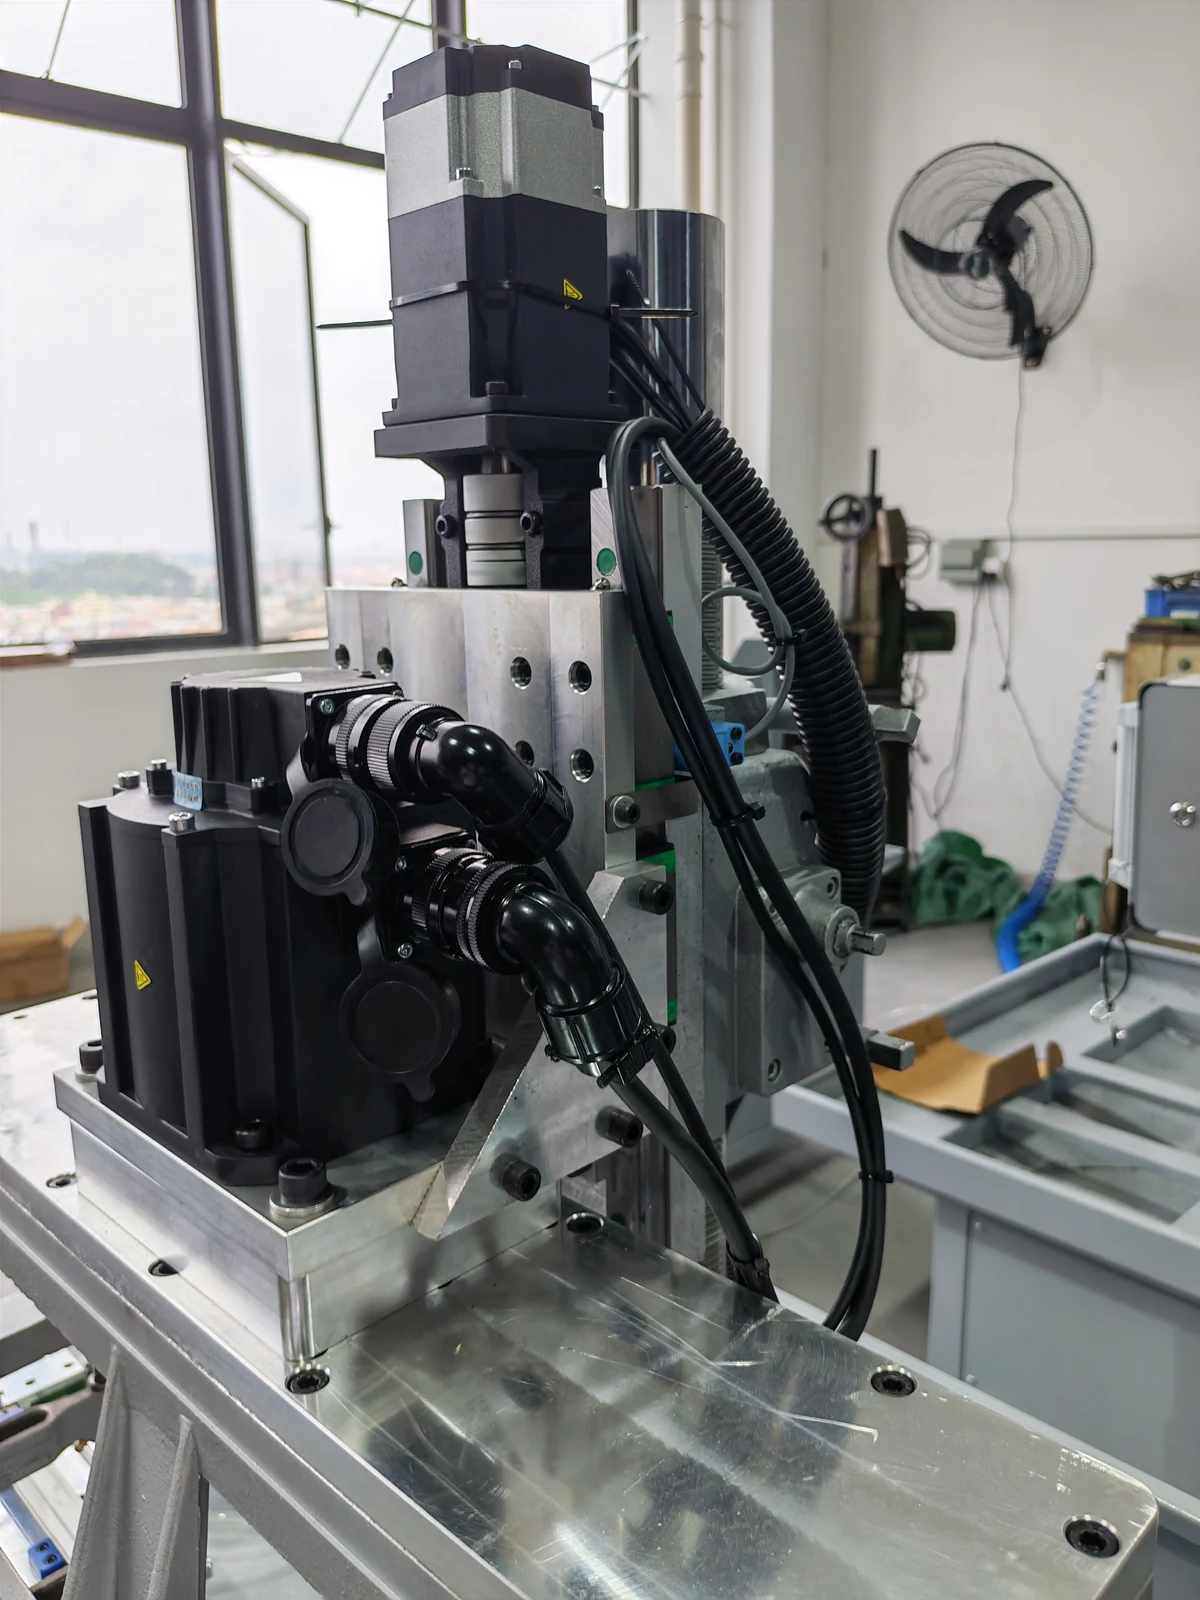
Servo feed drive
Close view of the servo feed assembly and adjacent spindle drive.
 View full-size image ↗
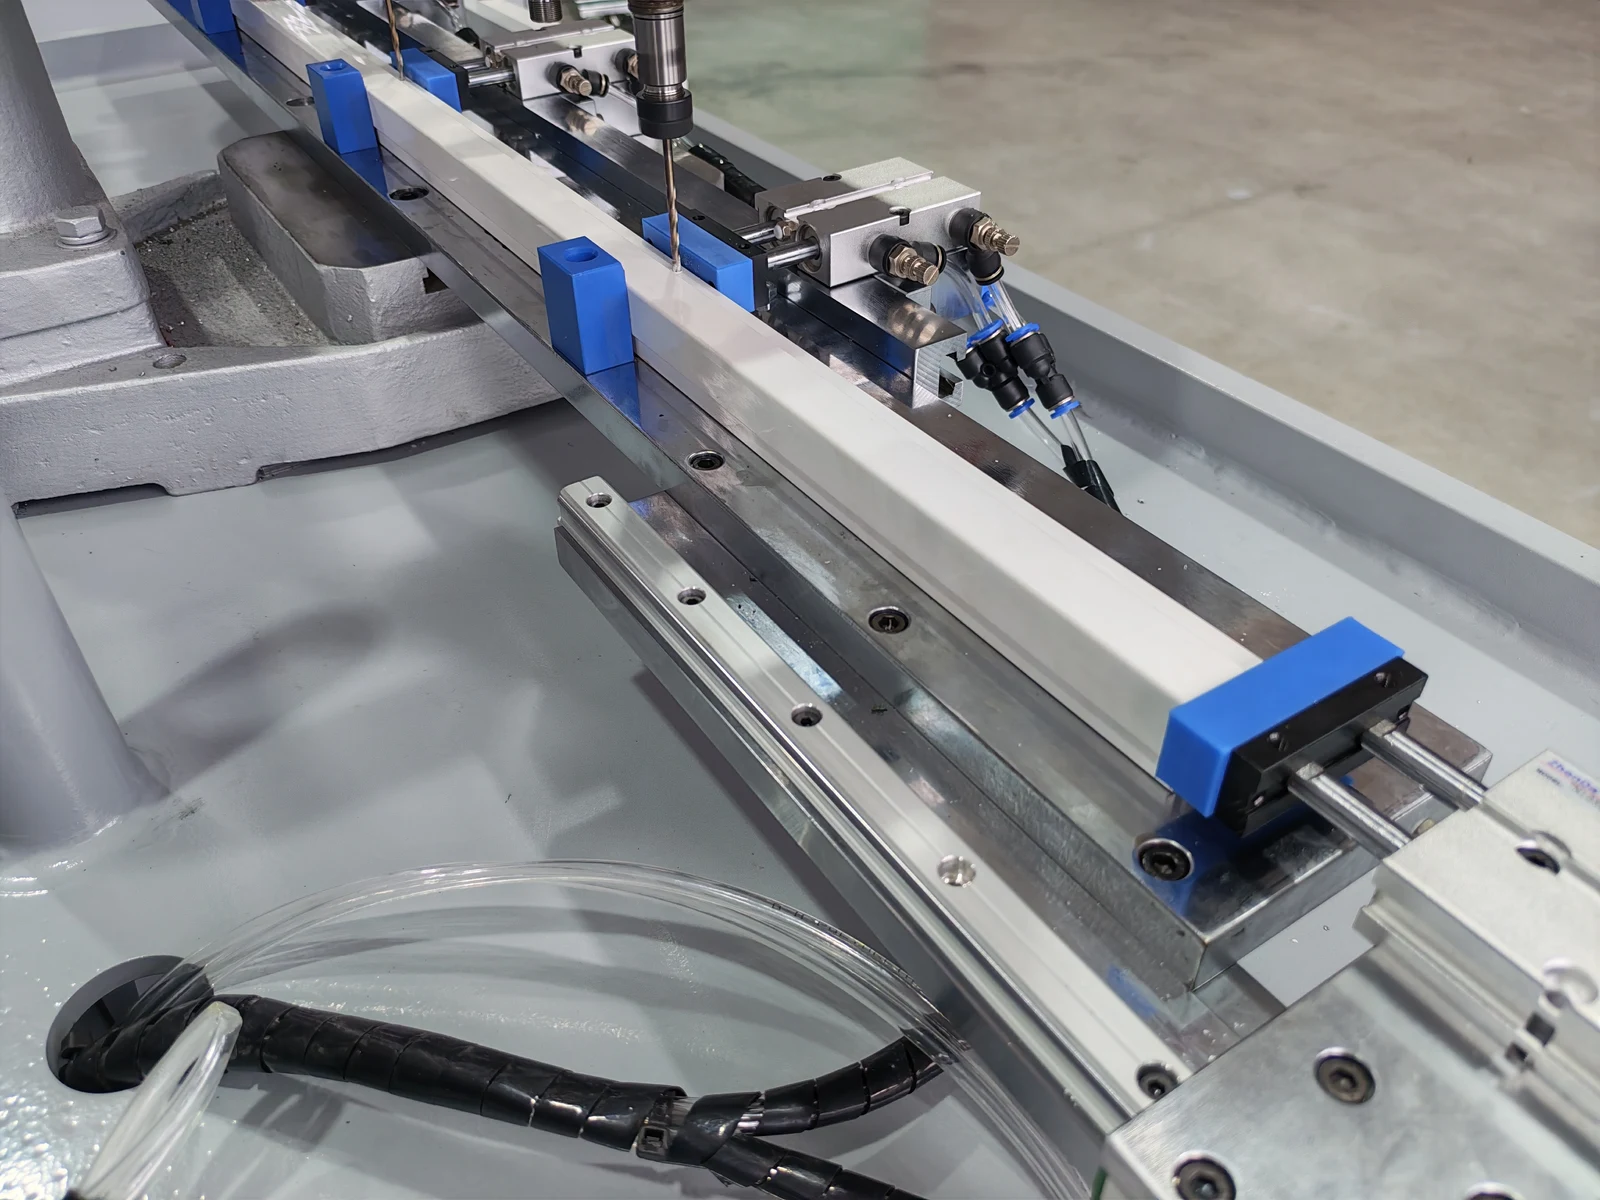
Servo-drive connections
Motor connectors and cable routing on the upper head assembly.
 View full-size image ↗
PVC profile fixture
PVC profile supported along the fixture with blue locating blocks.
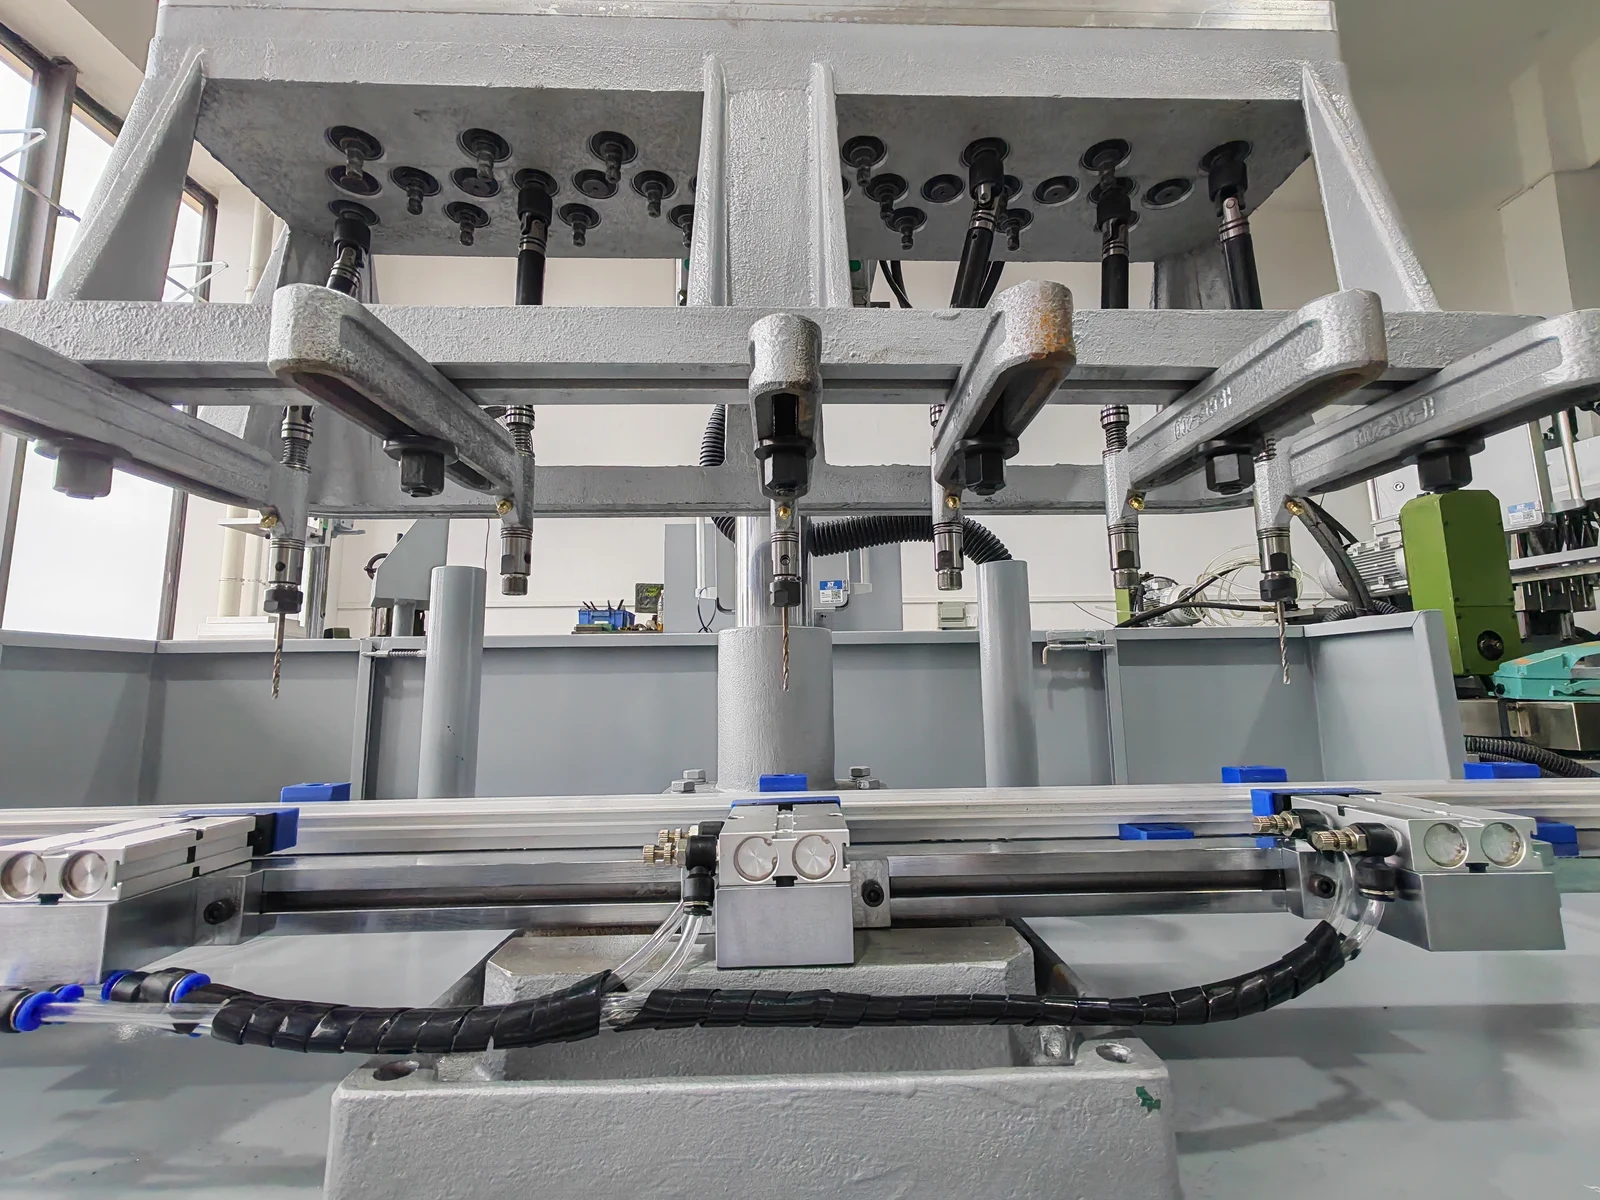 View full-size image ↗
Six-spindle head
Underside view of the drilling head and tooling arrangement.
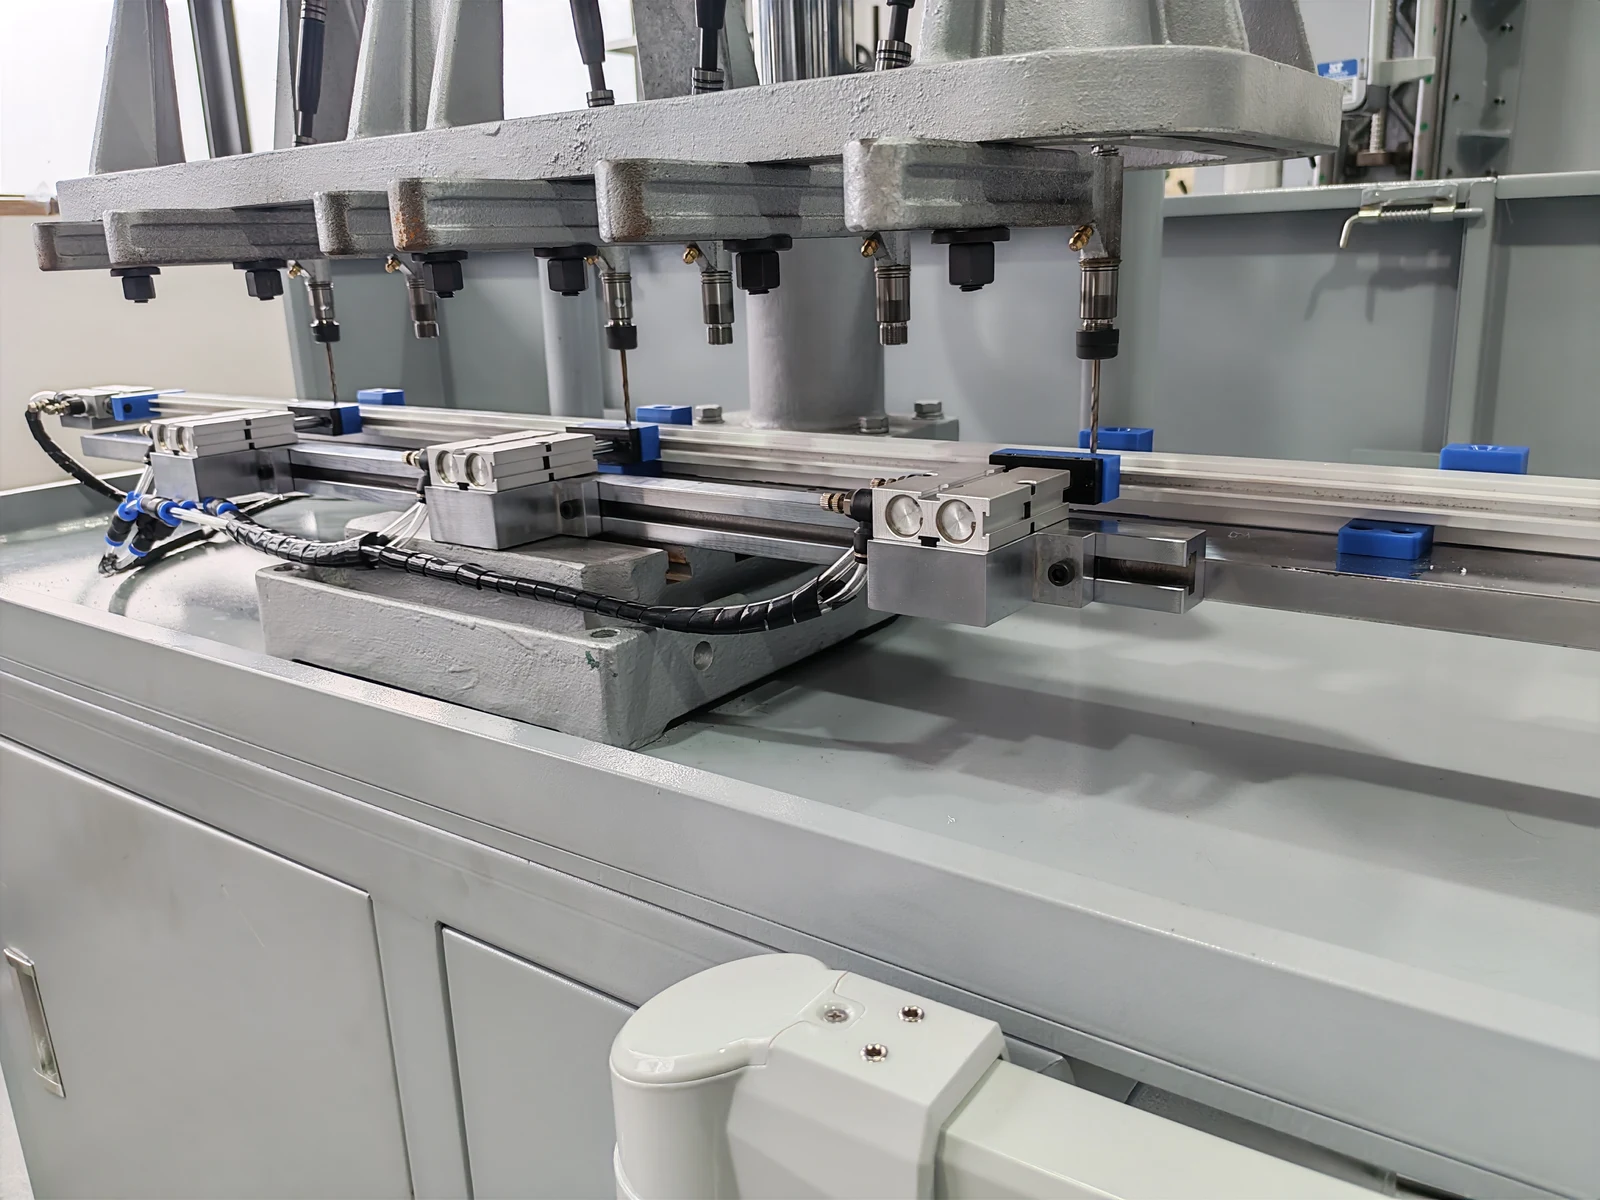 View full-size image ↗
Drilling station
Angled view of the tools, profile supports and pneumatic cylinders.
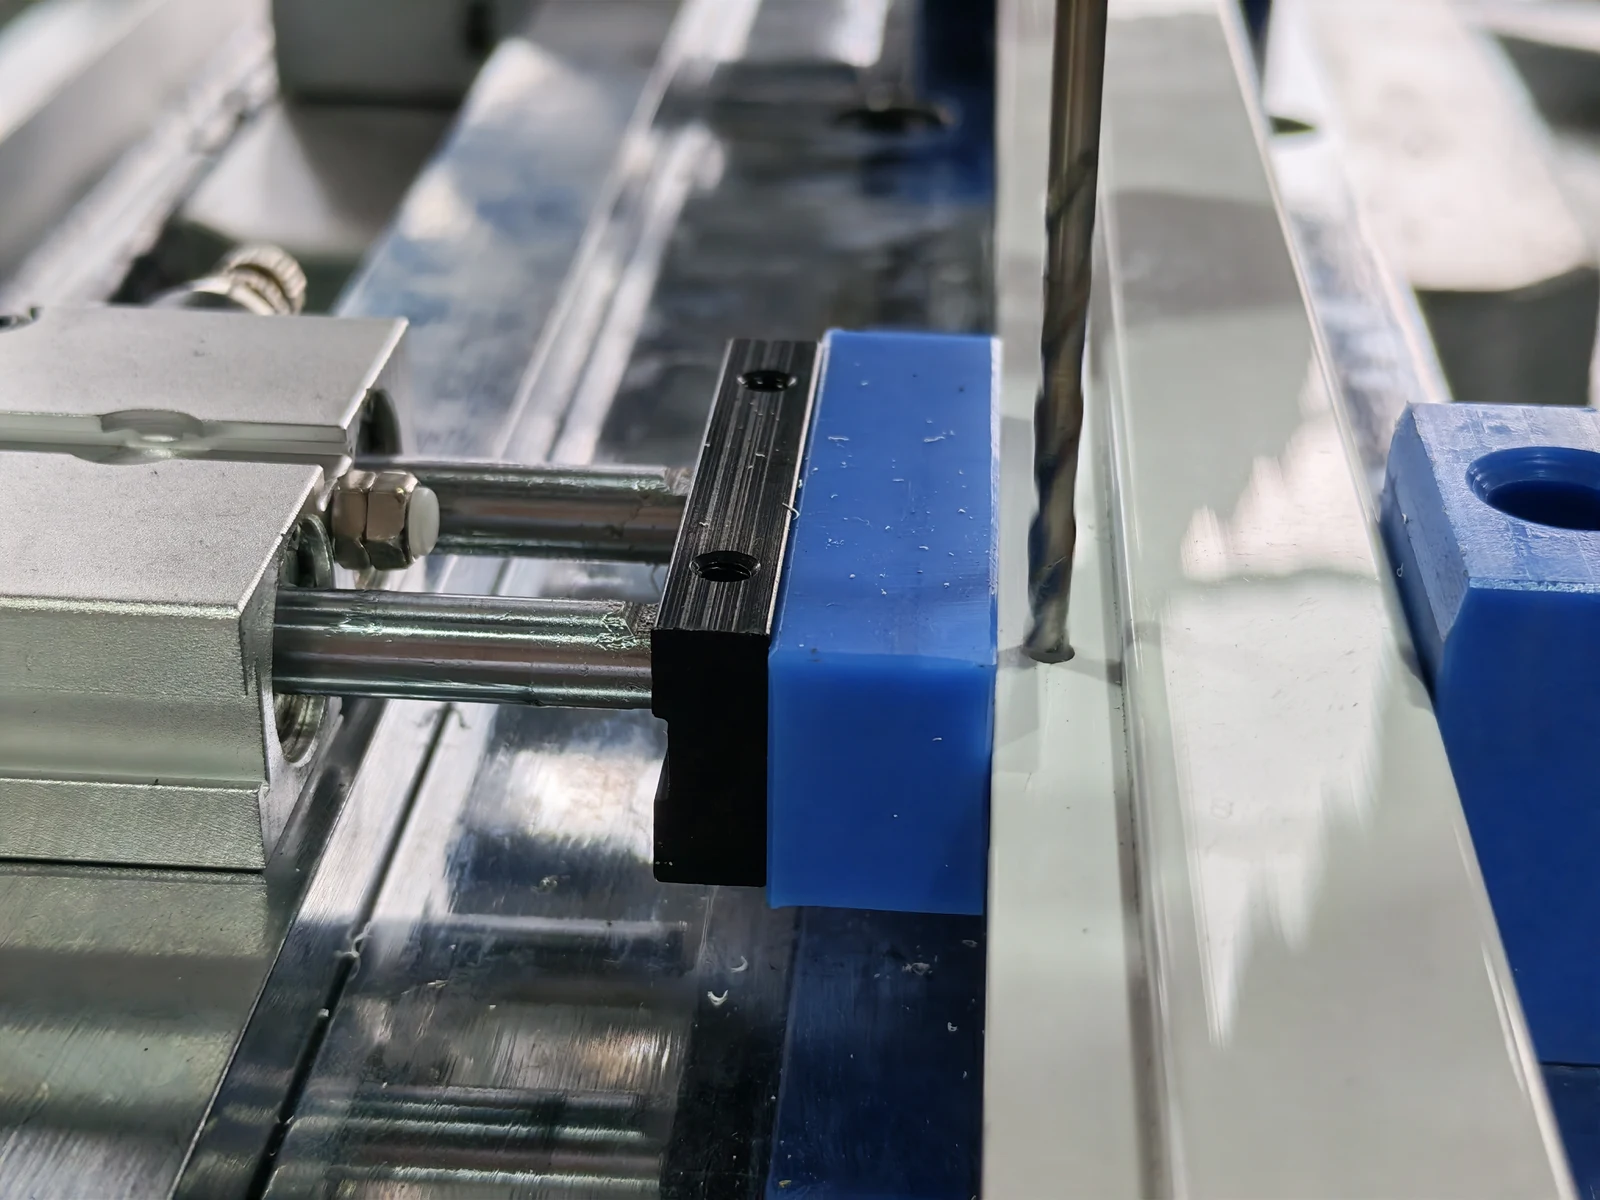 View full-size image ↗
Drill and fixture detail
Close view of a drilling position beside the fixture block.
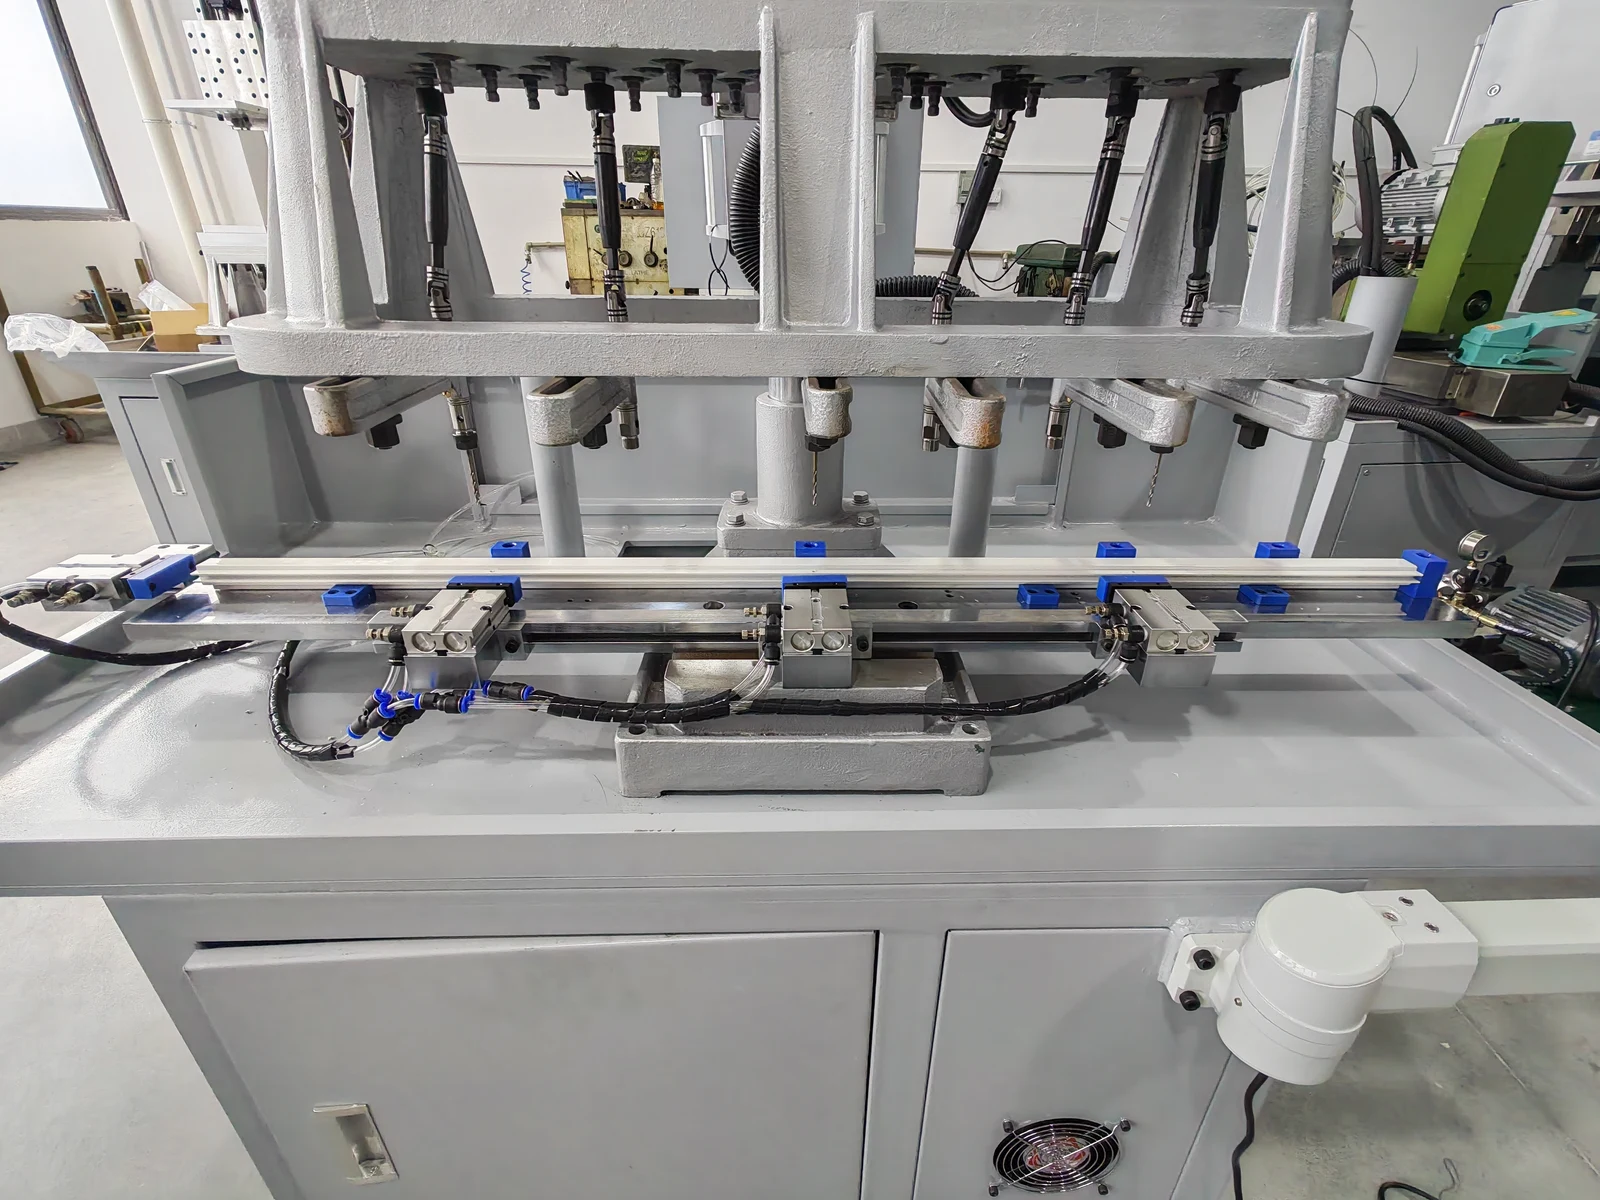 View full-size image ↗
Front fixture layout
Front view of the full fixture layout beneath the drilling head.
Project price reference
EXW price for the configuration shown
This reference relates to the six-spindle machine and its specified PVC workpieces. We review your part variants, hole patterns and handling requirements before quoting a corresponding configuration.
Production and commissioning of the photographed machine are complete. The quoted lead time below is measured from receipt of the deposit.
US$4,800
Quoted lead time: 12–15 days after receipt of the deposit.
We confirm the scope, price and lead time for your order in the quotation.
Request a QuotePlan your application
Need several holes drilled in your PVC parts?
A drawing is useful, but clear part photos and a description are enough to start the conversation.
Discuss Your PartUseful details to share
- Drawings or clear photographs of each part variant
- PVC specification, cross-section and workpiece length
- Hole diameters, positions, depths and tolerances
- Required output and preferred loading method
The selected machine or solution will be included in your inquiry.