Standard machine · BX-4508V

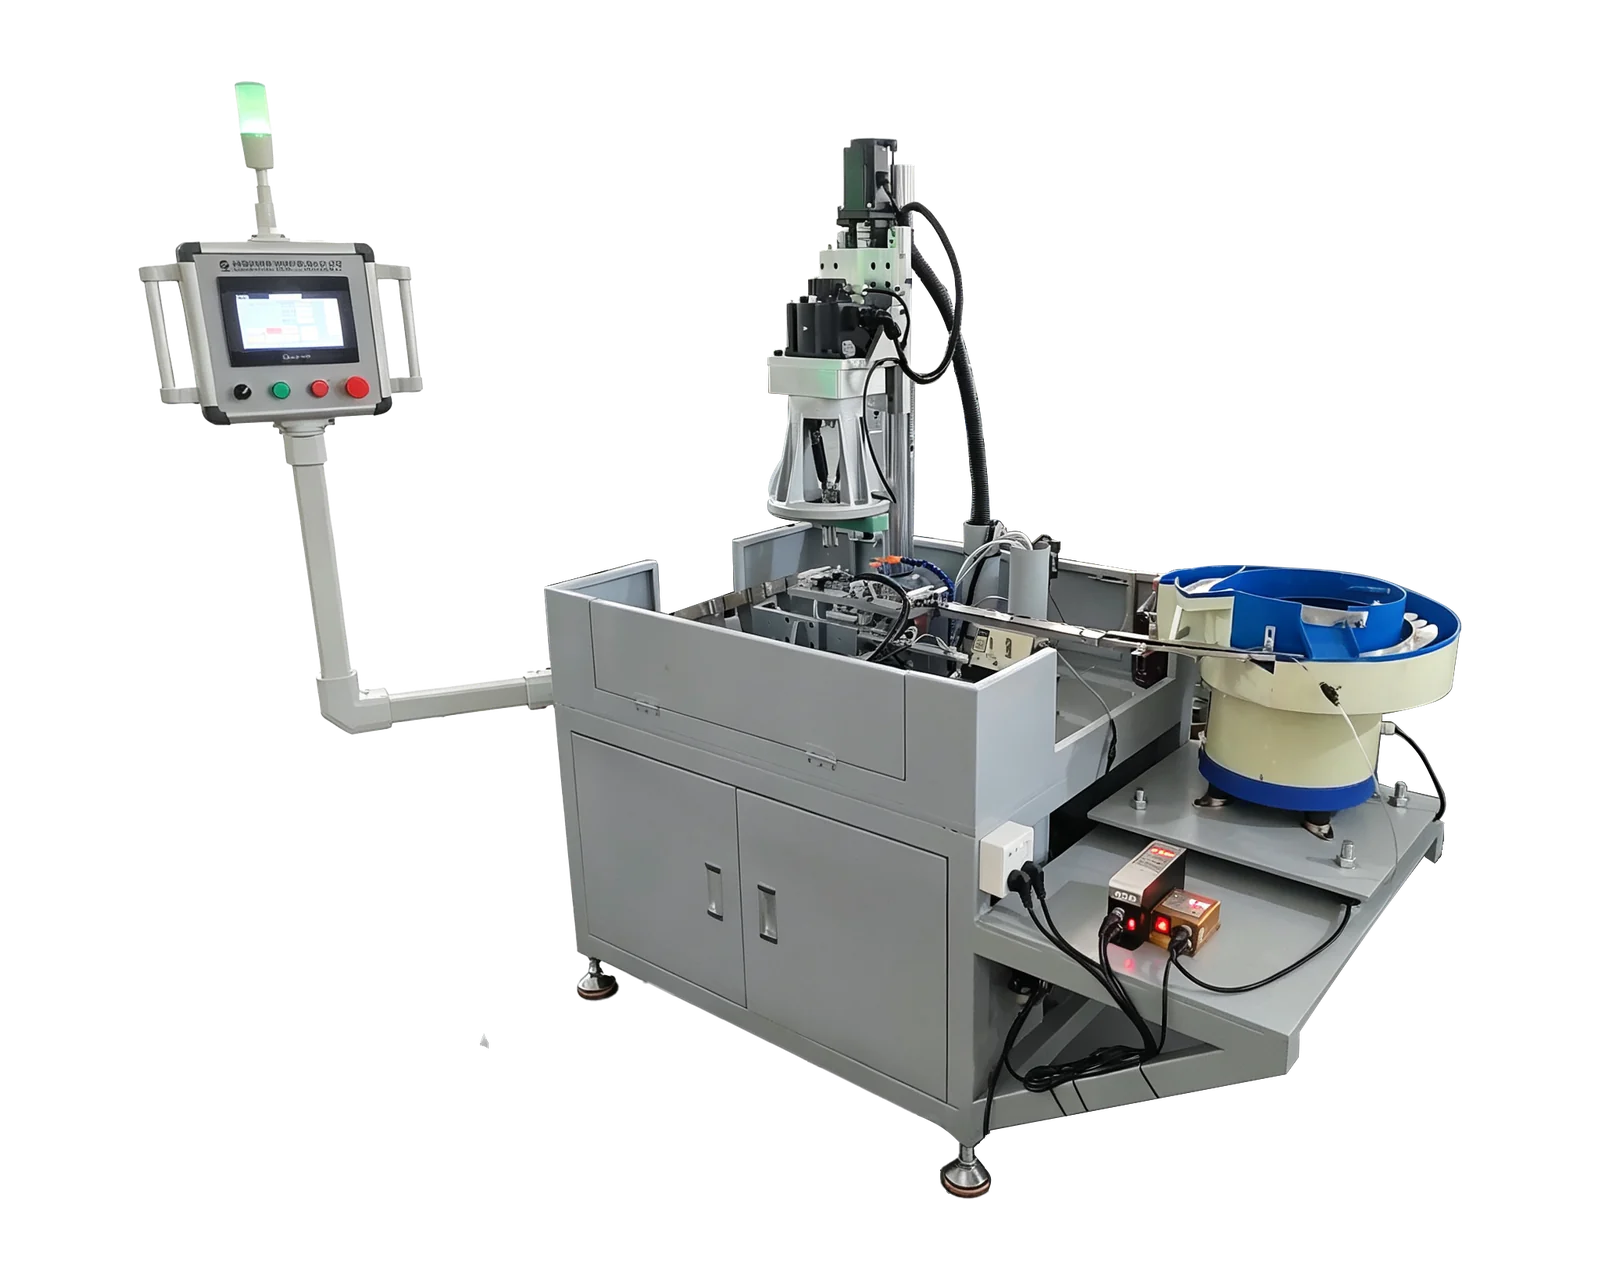
BX-4508V Gear-Driven Automatic Tapping Machine

A gear-driven tapping machine for repeated internal threads in prepared holes. Match the pitch gearing, tap, holder and fixture to your part. Review the BX-4508V when the tapping task is defined; include every thread variant and the supplied-hole condition in your inquiry.

  • Tapping
  • Gear-driven feed
BX-4508V gear-driven tapping machine
Standard machine · BX-4508V

Define your configuration

Define the thread and pitch-gearing setup

Start with the holes as they arrive at the tapping station. The quotation should connect each thread requirement to an identified gearing, tooling and workholding arrangement.

Proposed process functions and questions to resolve
FunctionScope to reviewConfirm for your part
Thread scheduleIdentify every thread size, pitch and required usable depth.Metric or inch designation, tolerance and part variants
Pitch gearingConfirm the gearing supplied for each intended pitch and how changes are made.Included gear sets, change procedure and setup check
Prepared holeDefine the input to tapping, including work completed upstream.Bottom-hole specification, entry condition, through/blind detail and depth reference
Tap and holderReview the selected tool with the machine feed and the workpiece.Tap identification, holder interface, projection and available clearance
Fixture and loadingSpecify how the part is located, clamped, loaded and removed.Locating surfaces, protected areas, manual handling or separate feeding scope

Scroll horizontally to compare all columns on smaller screens.

The published M1–M8 range is a platform reference. It does not establish suitability for every stainless steel, brass or aluminum part, or for every multi-spindle load. Tooling, material condition, hole geometry and the proposed setup require application review.

01

Repeated pitch or frequent changeovers

List the pitches and batch sequence before comparing gear-driven and servo tapping. Ask which gears, tools and fixtures change, who performs the setup and how the first part is checked. Drive type alone does not establish total changeover time.

02

Blind-hole requirements

Provide usable thread depth separately from prepared-hole depth, including the drawing reference and bottom geometry. Ask the supplier to confirm tool travel, reversal, clearance and cleaning for the selected tap. Do not substitute a universal bottom allowance.

03

Single or multi-spindle tapping

For several holes, include coordinates, pitches and tool clearances. A multi-spindle head is an application-specific option; the proposal must define the active tools and compatible feed arrangement. Mixed pitches are not automatically supported in one shared stroke.

Catalog reference

Reference specifications

These catalog values describe the machine platform. Confirm the applicable range for your material, spindle count, tooling and machining requirements before ordering.

BX-4508V platform reference
Catalog modelBX-4508V
Tapping rangeM1–M8
Spindle stroke45 mm
Motor power0.75 kW
Head adjustment0–260 mm

Machine operation

Watch related equipment videos

Use these equipment examples to review the layout and operation. Tooling, workholding and the machining sequence must be agreed for your part.

4508 Gear-Driven Automatic Tapping Machine
STANDARD MACHINE / VIDEO

4508 Gear-Driven Automatic Tapping Machine

A gear-driven tapping platform for repeated thread machining. Select the pitch gearing, tooling and fixture for your workpiece.

View machine platform →

Price & quotation

Request a price for a defined equipment scope

BX-4508V tapping machine price depends on the included pitch gearing, tap holders, tooling, fixture and any multi-spindle head. List drilling, loading and inspection separately so a tapping-station quote is not mistaken for a complete production cell.

  • Part drawing and thread schedule for every variant
  • Material grade, supplied condition and prepared-hole specification
  • Usable thread depth, blind-hole geometry and inspection requirement
  • Required pitch gear sets, tooling and fixture scope
  • Loading preference, target output, destination and electrical supply

Before ordering

Questions to resolve for your part

Does the BX-4508V drill the hole before tapping?

This platform is listed for gear-driven tapping. Define how the prepared hole is supplied. If drilling or chamfering must be included, request a complete process review and compare the dual-servo or custom layouts; do not assume those operations are included here.

Can it tap stainless steel or blind holes?

Submit the exact grade, material condition, thread and hole geometry for review. The catalog range does not confirm a material-specific capacity or a bottom clearance. Ask for the proposed tooling and representative-part trial scope before accepting an application claim.

Are metric and inch pitches included?

Metric or inch pitch gearing is listed as an option. The quotation should identify the actual supplied pitches and gear sets, plus the change procedure. A general option listing does not mean every required pitch is included.


Continue your review

Guides for the next decision

Related custom layouts

Need a more integrated process?

Explore these alternatives when a dedicated station layout, feeding arrangement or machining sequence is part of the requirement.

Combine repeated operations in one indexed sequence

Rotary Indexing

Move parts between drilling, chamfering and tapping stations on a rotary layout. Station count, tooling and loading are designed around the workpiece.

  • Drilling
  • Chamfering
  • Tapping
  • Indexing
Explore solution

Feed, position and machine repeated small parts

Automatic Feeding

Combine part feeding, positioning and machining in a dedicated cell. Feeding suitability depends on the shape, orientation and surface condition of the workpiece.

  • Part feeding
  • Tapping
  • Unloading
Explore solution